Technical Specifications
Product Overview
High-Efficiency Welding Electrode
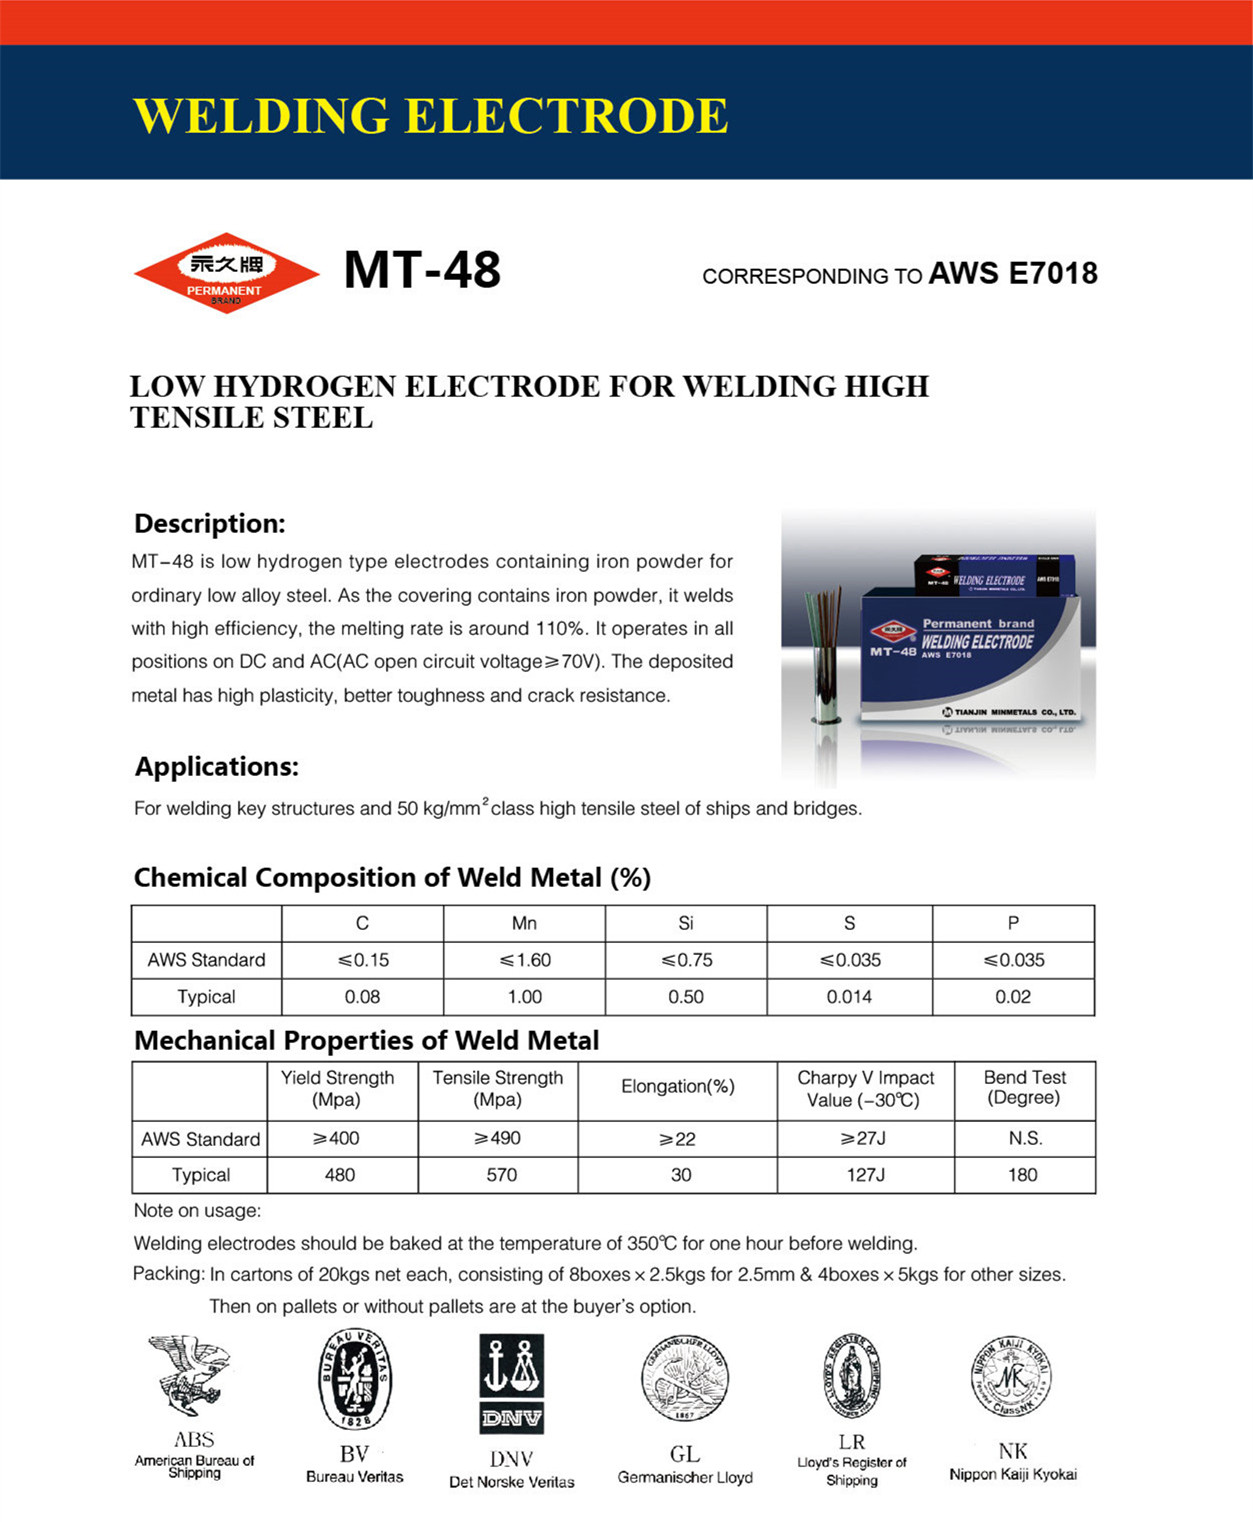
This low-hydrogen welding electrode is formulated with iron powder, designed specifically for welding ordinary low alloy steel. It offers high operational efficiency with a melting rate of approximately 110%, ensuring consistent and reliable performance. The deposited metal provides excellent plasticity, toughness, and crack resistance, making it suitable for critical structural applications including ships and bridges.
Technical Specifications
- Welding Positions
- All Positions
- Current Type
- DCAC (Open circuit voltage ≥70V)
- Melting Rate
- 110 %
- Baking Requirements
- 350°C for 1 hour before use
Chemical Composition
Chemical Composition of Weld Metal (%)
| Element | Standard Max (%) | Typical (%) |
|---|---|---|
| Carbon (C) | ≤0.15 | 0.08 |
| Manganese (Mn) | ≤1.60 | 1 |
| Silicon (Si) | ≤0.75 | 0.5 |
| Sulfur (S) | ≤0.035 | 0.014 |
| Phosphorus (P) | ≤0.035 | 0.02 |
Mechanical Properties
Mechanical Properties
| Property | Standard | Typical |
|---|---|---|
| Yield Strength (MPa) | ≥400 | 480 |
| Tensile Strength (MPa) | ≥490 | 570 |
| Elongation (%) | >22 | 30 |
| Charpy V Impact (-30℃) | ≥27J | 127J |
| Bend Test (Degree) | N.S. | 180 |
Logistics & Packaging
Packaging Details
- 20kg net carton weight
- 8 boxes x 2.5kg (for 2.5mm electrodes)
- 4 boxes x 5kg (for other sizes)
- Pallet options available upon request
Certifications
Industry Approvals
ABSBVDNVGLLRNK