Technical Specifications
Overview
Advanced Air Separation Solution
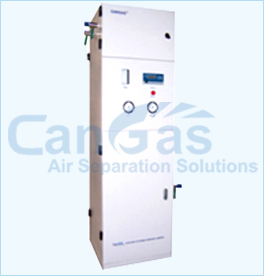
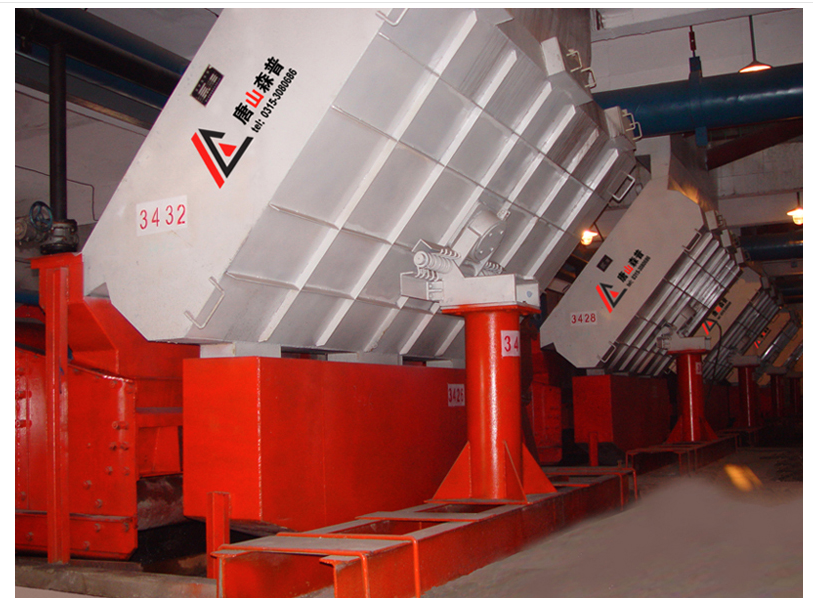
This advanced air separation unit is specifically engineered for high-performance chemical processing environments. It features precise control and monitoring systems to ensure efficient gas separation, significantly enhancing productivity and operational safety. Designed with a compact footprint and integrated components, the system allows for seamless operation and minimal maintenance requirements.
Key Features
Operational Benefits
- Precise control and monitoring systems
- Compact design for space efficiency
- Integrated components for seamless operation
- Low maintenance requirements
- Primary Function
- Nitrogen GenerationAir SeparationChemical Processing
Application
Industry Suitability
Chemical ManufacturingIndustrial Gas Processing