Technical Specifications
Overview
Industrial Chemical Reactor
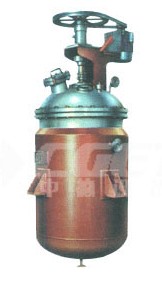
This industrial chemical reactor is engineered for demanding chemical processing environments, facilitating precise mixing, heating, and reaction control. Featuring a robust closed-vessel design, it includes a high-performance agitator mechanism powered by a top-mounted motor. Equipped with multiple dedicated ports, it allows for seamless reactant addition and real-time monitoring, making it an ideal solution for both batch and continuous chemical synthesis operations.
Key Features
Design & Construction
- Closed vessel architecture
- Top-mounted agitator motor
- Multi-port configuration for reactant intake
- Integrated monitoring ports
- Core Functionality
- MixingHeatingReaction ControlBatch SynthesisContinuous Synthesis
Operational Metrics
Operational Capabilities
1 Top
Agitator Motor Position